
1.1 Handbook Purpose and Organization
The purpose of this Asphalt Paving Handbook is to provide comprehensive technical information and best practices related to the paving of asphalt mixtures for both roadway and airfield projects. The goal is to keep the discussion focused on practical aspects that have the greatest effect on the quality and long-term performance of the finished pavement.
Asphalt paving success cannot be accomplished with simply good paving and compaction operations. Success also depends on appropriate structural design, proper materials selection, mix design, plant production, surface preparation, and quality assurance (QA). Using best practices in each of these phases results in asphalt pavements that are built to last.
The Airport Asphalt Pavement Technology Program (AAPTP), a cooperative effort between the National Asphalt Pavement Association (NAPA) and the Federal Aviation Administration (FAA), produced this Handbook for those involved in asphalt paving production, construction, and QA programs. This includes personnel representing the contractor, user agency or owner, and consultants. In particular, the target audience includes inspectors, project engineers, designers, superintendents, foremen, paving crews, plant operators, and testing technicians.
This Handbook’s target audience includes inspectors, project engineers, designers, superintendents, foremen, paving crews, plant operators, and testing technicians.
The Handbook’s discussion of referenced specifications and test methods is current as of the publication date. Readers should review current specifications to ascertain any pertinent changes that may have occurred since that time.
The first edition of this Handbook was published in 1991 by the Transportation Research Board with financial support from the American Association of State Highway and Transportation Officials (AASHTO), FAA, the Federal Highway Administration (FHWA), NAPA, and the U.S. Army Corps of Engineers (USACE). In 2000, the National Research Council appointed a committee of experts from agencies, producers, and contractors to update the Handbook. Since its inception, the Handbook has served as a longstanding, venerable reference used across the asphalt paving industry to promulgate good practices. This current edition provides a much-needed update to incorporate the latest technology, equipment, methods, and standards.
The organization of this latest edition has changed substantially from previous editions, now consisting of 12 chapters covering the process of an asphalt paving project from start to finish. This Handbook includes many “between chapter” references where topics have different aspects covered in multiple chapters. Referencing the discussion in other chapter(s) minimizes duplicate discussions.
Following this Chapter 1 introduction, Chapter 2 provides a brief review of project organization. The role of materials and the mix design relative to mixture behavior is covered in Chapter 3. A discussion of how the mix design performed in the lab will likely differ from the mix produced in the field also occurs in Chapter 3, including some discussion of the adjustments that will be needed.
Mix production at the plant is covered in Chapter 4 in a more abbreviated manner than previous editions of the Handbook to keep it proportional with other topics. Chapter 5 covers the proper preparation of the surface to be paved over, whether it be a new granular base or an existing asphalt or concrete pavement. This includes details on prime coats and tack coats. Delivery of the mixture from the plant to the jobsite is covered in Chapter 6, including equipment types and proper loading and unloading procedures.
Chapter 7 discusses mix placement on the jobsite. The chapter covers equipment, procedures, and grade and slope control, including automation. Chapter 8 is a thorough discussion on compaction of the mat, including roller types, factors that affect compaction, and establishing a rolling pattern. Both longitudinal and transverse joints are discussed in Chapter 9, with heavy emphasis on best practices for placing and compacting joints.
Chapter 10 has been added to provide a dedicated and more thorough discussion on the critical topic of segregation, including possible sources and corrective measures. Chapter 11 covers the complex topic of QA, providing essential fundamentals for the many ways an agency approaches quality control (QC) and acceptance in its specifications and procedures. Finally, Chapter 12 focuses on the many possible mat problems that may occur, in addition to segregation as covered in Chapter 10.

To complement the written guidance in this Handbook, the AAPTP produced a series of 30 videos highlighting key topics covered in the chapters. Filmed at active airfield projects across the United States, these 3- to 5-minute videos demonstrate best practices in the field and feature perspectives from industry professionals. A video icon next to a chapter or section heading signals when a related video is available. A complete list of the videos, with direct links, is provided in the Appendix.
1.2 Airfield Paving
The earlier editions (1991 and 2000) of this Handbook focused on roadway paving. A major change in this new edition is greater emphasis on airfield paving, with additional discussion on practices unique to airfield work. The differences between roadway and airfield standard practices are covered on a topical basis as warranted throughout the Handbook, not necessarily as separate sections but as expanded discussion. References may be made to both the FAA and Department of Defense (DoD) airfield paving standards and specifications.
A major change in this new edition of the Handbook is that it places greater emphasis on airfield paving, with additional discussion on practices unique to airfield work.
The FAA’s standard asphalt paving specification for airfields is Item P-401 found in advisory circular 150/5370-10H. The DoD’s standard asphalt paving specification for airfields is Unified Facilities Guide Specification (UFGS) 32 12 15.13. While these two airfield specifications have some similarities regarding materials, gradations, joints, etc., they also contain many differences, especially concerning QC and acceptance.
For several reasons, airfield pavements provide unique challenges compared to roadway pavements, and these challenges affect the paving process.
First, the tire pressures of aircraft wheels are much greater than those of truck tires. Large commercial aircraft have tire pressures ranging from 150 to 250 pounds per square inch (psi), while large trucks have tire pressures ranging from 85 to 110 psi. Military fighter aircraft can have tire pressures that exceed 300 psi. These extremely high tire pressures, especially when combined with slow-moving or standing loads, can cause a newly paved asphalt surface to be prone to rutting, shoving, or scuffing unless the mix is designed, produced, placed, and compacted in a manner that ensures sufficient stability.
A second reason is that airfield pavements must be designed, constructed, and maintained in a manner that does not produce foreign object debris (FOD), a term very familiar to those involved in airfield pavements and operations. FOD is any debris that can be ingested in a jet engine and cause damage, leading to major flight safety concerns as well as costly engine repairs. Because of FOD concerns, airfield pavements must be kept at a higher serviceability level than highway pavements.
A third reason is that paving on airfields (shown in Figure 1) drastically disrupts airfield traffic operations compared to traffic disruption caused by roadway paving. For most highway paving, traffic can be diverted but remain open by closing one or a few lanes. For airfield paving, the entire runway or taxiway must typically be closed because closing partial width on a runway or taxiway to keep traffic open is not an option.
A fourth reason is that airfield specifications typically have very stringent smoothness requirements, so the paving process requires more attention than “everyday” roadway paving.
All these reasons and more explain why paving on airfields is referred to as the “high-wire act” of asphalt paving.
The FAA’s standard asphalt paving specification for airfields is Item P-401 found in advisory circular 150/5370-10H. The DoD’s standard asphalt paving specification for airfields is Unified Facilities Guide Specification (UFGS) 32 12 15.13.
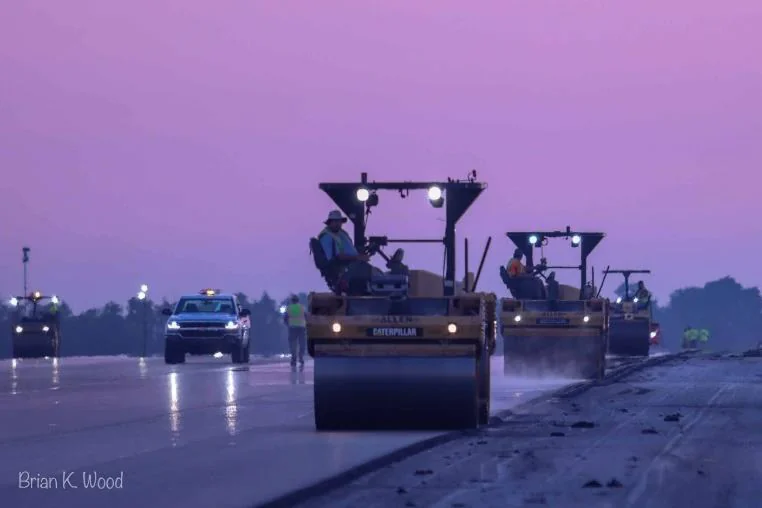
Figure 1. Roller Train Ensuring Compaction on a Runway Project
1.3 Asphalt Mixtures Defined and Classified
Asphalt mixtures consist of aggregate and asphalt binder that are precisely blended and mixed in an asphalt plant and then placed and compacted on the jobsite, typically in multiple lifts.
The term “asphalt mixtures” is used generically to include the many different types of aggregate and asphalt binder mixtures (also referred to as bitumen, asphalt, or asphalt cement) produced in an asphalt plant. Traditionally referred to as “hot-mix asphalt” (HMA), the change in terminology to “asphalt mixtures” was spurred by the introduction of warm-mix asphalt (WMA). WMA is a generic term for various products and technologies incorporated into asphalt mixtures that allow for decreased mix temperatures while maintaining the workability needed for mixing, paving, and compaction. Asphalt mixtures include HMA and WMA.
A wide range of mixture additives and binder modifiers can be used in a particular asphalt mix design. Both categories are discussed in Chapter 3.
Mixtures can be classified and produced with a wide range of aggregate types, sizes, and combinations, each having its own characteristics suited for a specific design application. Mix types vary depending on the performance demands of that layer (lift or course) in the overall pavement structure. Layer names or terminology can vary by agency, region of the country, etc. In general, base course refers to the bottom asphalt layer, intermediate course refers to a middle layer, and surface or wearing course is the top layer. Thinlay is a term used for a thin overlay of the surface. In general, larger aggregate sizes with lower binder contents are used in lower lifts, while smaller aggregate sizes with higher binder contents are used in lifts toward and at the surface. Mixes incorporating larger aggregates do not necessarily possess higher strength, as discussed in Section 3.3.1.
While each agency may have its own unique mix designations, several ways to categorize and name the various types of asphalt mixtures are common. The first is by designating the nominal maximum aggregate size (NMAS) of the aggregate used in the mix. This is covered in Chapter 3. The second is by gradation type, of which there are three: dense graded, open graded, and gap graded. Some agencies also include binder grade in their mix designation. An example of a mix designation for an agency is “12.5 mm Superpave with PG 64-22.”
Dense-graded mixes use an aggregate gradation that is well-distributed throughout the entire range of aggregate particle sizes used, from coarse through fine, resulting in a “dense” aggregate packing structure. Superpave and Marshall are the predominant mix design methods (discussed in Chapter 3) that produce dense-graded mixes. Dense-graded mixes are by far the most common mix type used on roadways and airfields. A further way to categorize a dense-graded mix is by whether it is fine or coarse graded. This distinction is generally made by whether the gradation line falls above or below the maximum density line (MDL) on the 0.45 power curve, as discussed in Chapter 3. For example, a “19-mm fine” typically means the mix has a 19-mm NMAS with a fine dense gradation.
Open-graded mixes consist of an aggregate with primarily uniformly sized coarse particles and highly interconnected air voids. The primary purpose of these mixes is to serve as a drainage layer, either at the pavement surface or at the bottom of the structural pavement section. The surface drainage layer mixes are called open-graded friction course (OGFC) or permeable friction course. OGFCs are designed and placed as a surface course to provide a free-draining surface to prevent hydroplaning, reduce tire splash, and reduce tire noise. OGFC mixes typically have an NMAS of 12.5 mm or 9.5 mm. The second type of open-graded mix is called an asphalt-treated permeable base (ATPB). ATPBs are designed with low asphalt binder content and predominantly large-size aggregate, such as 25 mm or larger NMAS. ATPBs are placed at the bottom of the asphalt structure and tied to edge drains so any water that enters the structural pavement section, either from the surface or subsurface, can escape to the edge drains.
Gap-graded mixes consist of an aggregate gradation with larger and finer particles but little or no particles in the middle of the gradation band, which creates a “gap.” Stone matrix asphalt (SMA) is a common example of a gap-graded mix. SMA mixtures function similarly to dense-graded mixes in that they provide dense, impervious layers when properly compacted. They are known to be highly rut resistant due to their stone-on-stone aggregate structure and for their increased durability due to a thicker asphalt film coating the aggregate.
Section 3.3.1 in Chapter 3 has a complementary and more extensive discussion on particle size distribution, including illustrations of these three mix types by gradation as well as by NMAS.
1.4 Workmanship
Several major construction factors directly affect the ultimate performance of asphalt pavements: the structural design of the pavement layers; the binder, aggregate, and mix design qualities; the construction procedures used to produce, transport, place, and compact the mix; and the workmanship or quality of construction. Poor workmanship can be one of the most significant factors leading to premature distress of an asphalt pavement.
Causes of poor workmanship frequently include failure to comply with specifications, poor construction techniques, and improper equipment setup and operation. Appropriate training of construction personnel is key to good workmanship as well. Mix plant and paving train personnel must understand fundamental processes and procedures, as well as the consequences of failing to perform these best practices. For example, failure of roller operators to observe temperature zones during compaction could result in pavement areas that have low compacted density and risk premature pavement failures, translating to FOD on airfields.
To ensure pavements perform as expected, there is no substitute for careful adherence to best practices by all involved with asphalt paving in all phases of a project, as outlined in this Handbook.
Project management decisions can also lead to poor workmanship. For example, if paving is allowed to proceed during inclement weather, inadequate compaction can result despite proper practice by equipment operators. Similarly, if the paving operation moves too quickly, it can exceed the rate of delivery of material. This results in frequent stops of the paving train, which in turn can cause unnecessary pavement roughness and nonuniform density.
Proper performance of all construction-related tasks, including testing and inspection, ensures that the asphalt mixture produced, placed, and compacted will perform as expected. QC and acceptance procedures, such as those described in Chapter 11 of this Handbook, will identify instances of poor workmanship. These instances should be corrected as soon as possible. Chapter 12 of this Handbook is intended to help identify the causes of mat problems and offers recommended adjustments to prevent continuation of the problem.
There is no substitute for careful adherence to best practices by all involved with asphalt paving in all phases of a project, as outlined in this Handbook.
1.5 Certification and Accreditation Programs
Certification and accreditation programs are intended to increase the quality of construction by ensuring project team members and laboratories are knowledgeable about various topics in asphalt materials, sampling, testing, paving, QC, and acceptance. Certification applies to individuals, while accreditation or qualification applies to laboratories. Both are typically tied to an agency’s specific requirements and standards.
There are various certification programs across the United States. Many State agencies have their own certification programs for the various individual roles involved in an asphalt paving project, from sampling and testing technician to inspector to mix designer.
One example of a national certification program that has been adopted for military airfield projects is the Airfield Asphalt Certification Program (AACP). The three certifications available under the AACP are Laboratory Technician, QC Manager, and Inspector. Essentially, the UFGS 32 12 15.13 specification requires a contractor to have at least one individual with each of these certifications on their QC staff, and the individual must actively participate in that respective role during project execution.
AASHTO and ASTM International both offer national laboratory accreditation and proficiency programs. These programs are intended to increase proficiency and accuracy and reduce variability on certain laboratory tests.